Understanding Protective Coating Systems for Steel Pipe
Introduction
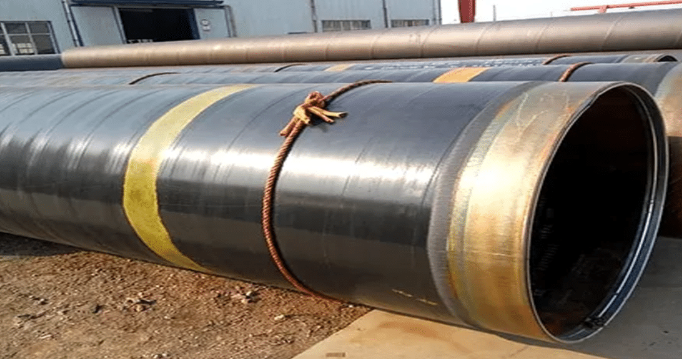
Steel pipe used in industrial and infrastructure applications may face exposure to moisture, soil, chemicals, and other environmental conditions. Protective coating systems can help provide a barrier between the steel surface and its surrounding environment.
For companies evaluating longma sfbe/dfbe pipe coating, understanding coating terminology, surface preparation, application procedures, inspection, and project requirements is important before selecting a system.
Why Steel Pipe Requires Protection
Steel can be affected by corrosion when exposed to suitable environmental conditions. In pipeline systems, corrosion control can therefore become an important part of asset planning.
A protective coating creates a physical barrier over the steel surface. Its effectiveness depends on appropriate surface preparation, coating application, curing, inspection, and handling.
The selected system should match the environment and project specification.
See also: Golden Retriever for Sale in California
Understanding FBE Coatings
Fusion bonded epoxy, commonly called FBE, is a powder-based coating system used on steel surfaces. During application, the powder is heated so that it melts and forms a continuous protective layer.
FBE is used in various pipeline and industrial applications where a protective coating is required.
The exact coating specification should be determined according to project requirements, including coating thickness, surface preparation, and testing.
Surface Preparation Matters
Even a technically suitable coating can perform poorly if the steel surface has not been properly prepared.
Surface preparation can involve cleaning the steel and creating an appropriate surface profile before coating application. The objective is to provide a suitable foundation for adhesion.
Manufacturers should control preparation conditions and verify the surface before proceeding with coating.
Application Conditions
Coating application needs controlled conditions to achieve consistent results. Temperature, cleanliness, application equipment, and powder characteristics can all be relevant.
The coating process should follow the applicable technical specification and established quality procedures.
Controlled application helps reduce defects and supports consistent coating thickness.
Inspection and Quality Control
Coated pipe should be inspected after application. Depending on the specification, inspection may include visual examination, thickness measurement, adhesion testing, holiday detection, or other applicable checks.
The exact inspection program depends on the coating system and project requirements.
Inspection records can provide useful documentation for quality assurance.
Consider the Operating Environment
The environment surrounding the pipeline should influence coating selection.
Underground pipelines may face soil and moisture exposure, while above-ground systems may encounter different environmental conditions. Temperature, chemicals, mechanical handling, and installation conditions can also be relevant.
The coating should therefore be selected according to the actual service environment rather than based solely on general product descriptions.
Handling After Coating
Coated pipe must be handled carefully to avoid damaging the protective layer.
Loading equipment, supports, lifting methods, and storage arrangements should be appropriate for coated products. Scratches or impact damage may require inspection and repair according to the applicable procedure.
Careful handling helps preserve coating integrity from the factory to installation.
Compare Coating Requirements
Before purchasing coated pipe, buyers should define:
- Coating type
- Surface preparation
- Coating thickness
- Application standard
- Inspection requirements
- Repair procedures
- Handling requirements
- Storage conditions
Clear specifications make supplier comparisons more straightforward.
FAQs
1. What is FBE coating?
FBE stands for fusion bonded epoxy. It is a powder coating system applied to prepared steel surfaces and used for corrosion protection in various applications.
2. Why is surface preparation important?
Proper surface preparation helps create a suitable foundation for coating adhesion and can contribute to consistent coating performance.
3. Should coated pipe be inspected after application?
Yes. Inspection can help identify coating defects, thickness variations, or other issues according to the project’s specified quality requirements.
Conclusion
Protective coating is an important consideration when steel pipe will be exposed to potentially corrosive environments. FBE systems provide one approach to protecting prepared steel surfaces, but successful performance depends on the complete coating process.
Surface preparation, application conditions, inspection, handling, and environmental requirements should all be included in the coating specification. A structured approach can help buyers and manufacturers maintain consistent coating quality.